


Double Block and Bleed Valve: A Critical Solution for Zero-Leakage Isolation
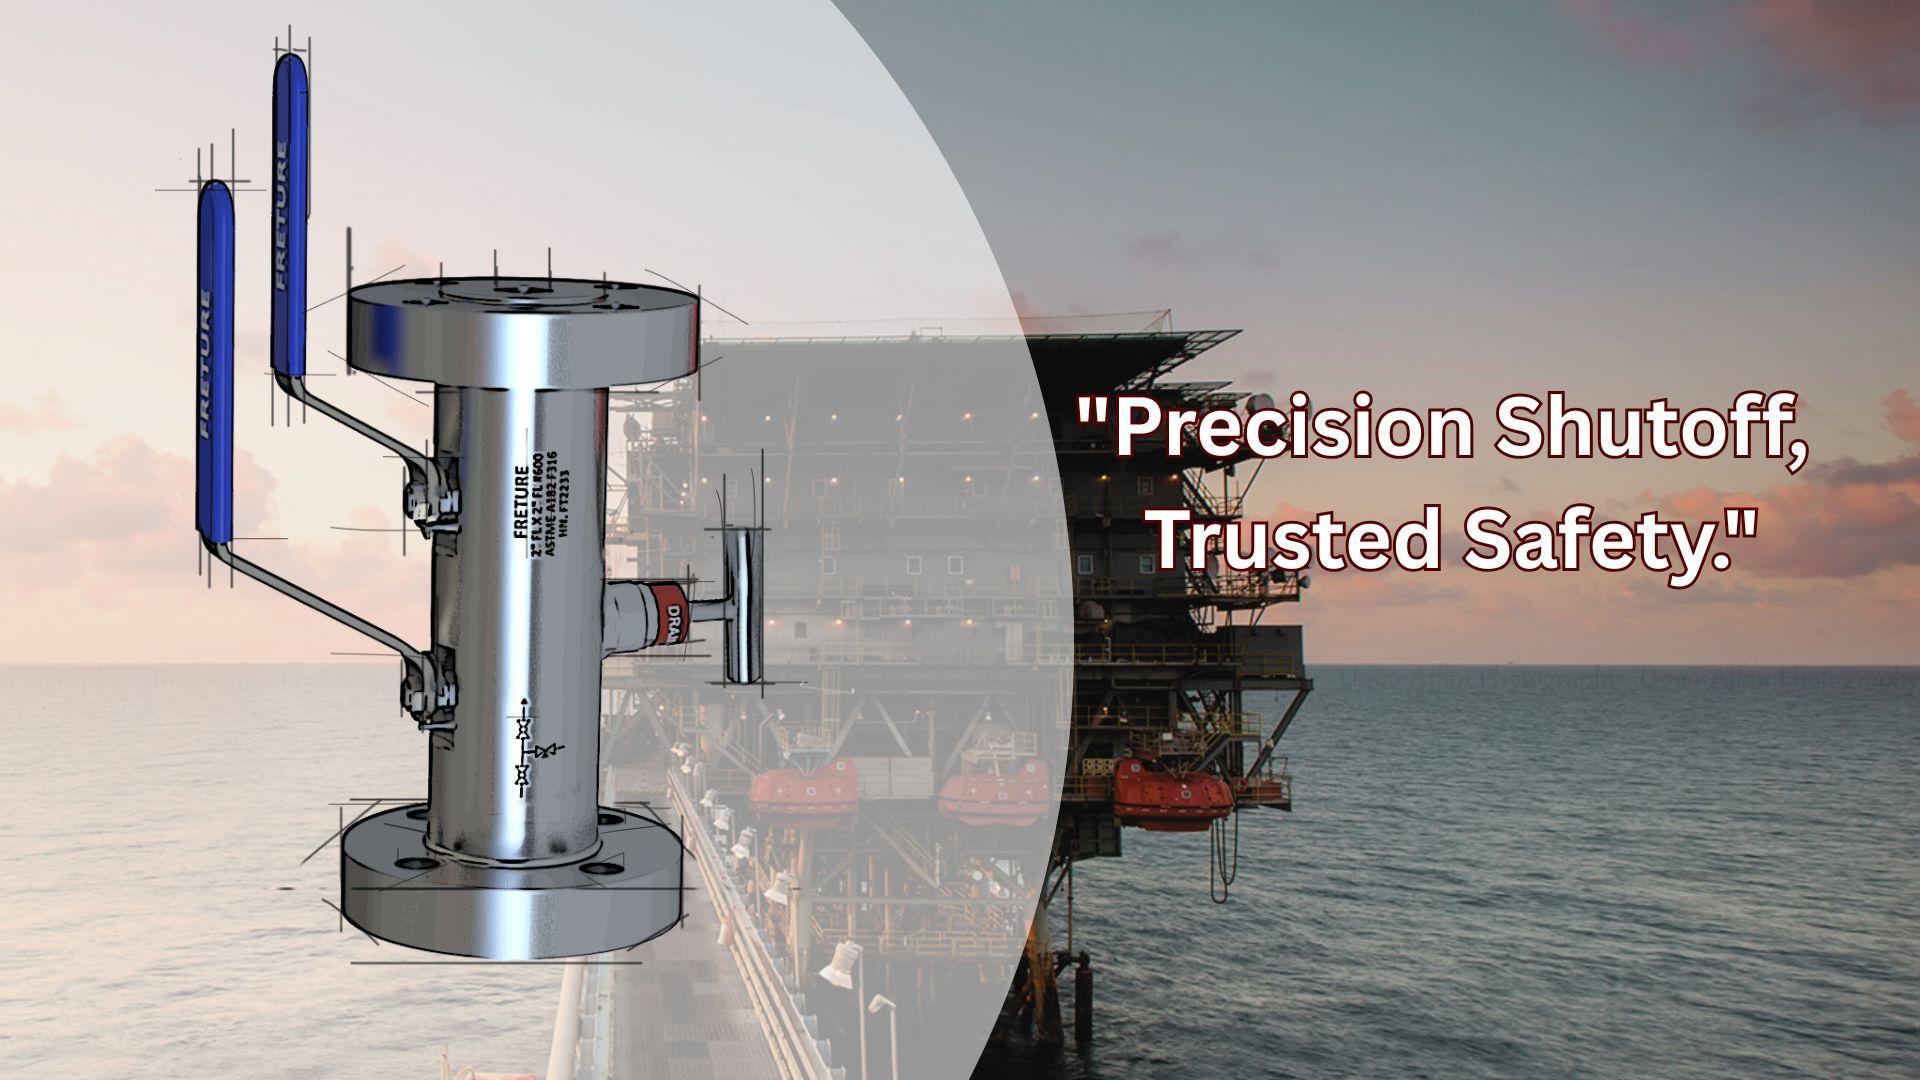
Industrial facilities handling hazardous or high-pressure fluids demand absolute control over flow isolation. In such environments, the Double Block and Bleed Valve (DBB Valve) has become a trusted solution for achieving safe and verifiable shutoff. Designed to prevent leakage and simplify maintenance, DBB valves are widely adopted across industries where operational safety and compliance are paramount.
Understanding the Double Block and Bleed Valve Concept
A Double Block and Bleed Valve integrates two independent sealing mechanisms within a single valve body, along with a bleed or vent port located between them. When closed, both seals isolate the process media from upstream and downstream flow. The bleed valve allows any trapped fluid or pressure in the cavity to be safely discharged.
This configuration ensures positive isolation, making DBB valves far more reliable than conventional single isolation valves used in critical service lines.
Operational Principle of DBB Valves
The operation of a DBB valve focuses on isolation verification. Once the main valve is closed, the bleed valve is opened to release residual pressure. If no fluid escapes, it confirms that both sealing elements are functioning correctly. Any leakage through the bleed port immediately signals seal degradation, enabling preventive maintenance before failure occurs.
This simple yet effective principle significantly reduces safety risks during line maintenance or equipment replacement.
Common Designs and Configurations
Double Block and Bleed Valves are available in various designs to match specific process requirements:
-
Single Ball DBB Valve – Features a floating or trunnion-mounted ball with two seats.
-
Twin Ball DBB Valve – Uses two separate balls to provide true double isolation.
-
Plug Type DBB Valve – Suitable for abrasive or high-temperature services.
-
Compact DBB Valve Assemblies – Replace traditional multi-valve manifolds, reducing installation space.
Selection depends on pressure rating, temperature range, media compatibility, and operational frequency.
Key Benefits of Using Double Block and Bleed Valves
The adoption of DBB valves offers several operational and economic advantages:
-
Superior Leakage Control – Minimizes the risk of fluid bypass.
-
Improved Personnel Safety – Ensures safe depressurization before maintenance.
-
Lower Installation Costs – Replaces multiple valves with a single unit.
-
Reduced System Complexity – Fewer joints mean fewer potential leak points.
-
Long-Term Reliability – Engineered for demanding industrial environments.
These benefits make DBB valves a preferred choice for safety-critical pipelines.
Applications Across Industries
Double Block and Bleed Valves are extensively used in industries where leakage can result in severe operational or environmental consequences:
-
Oil and gas production and transmission
-
Refineries and petrochemical complexes
-
Chemical processing plants
-
Power generation facilities
-
Offshore and subsea installations
-
Specialty and hazardous fluid handling systems
Their ability to ensure tight shutoff and verified isolation supports compliance with strict industry regulations.
Materials, Pressure Ratings, and Standards
DBB valves are manufactured using high-grade materials such as carbon steel, stainless steel, alloy steel, and duplex steel, allowing them to withstand extreme pressures and temperatures. They are designed in accordance with international standards including API 6D, ASME B16.34, ISO 15848, and fire-safe certifications, ensuring consistent performance and safety.
Importance of DBB Valves in Modern Process Engineering
As industries focus on reducing emissions, preventing leaks, and improving plant safety, Double Block and Bleed Valves have become an essential component in modern process engineering. Their compact design, combined with enhanced sealing capability, supports efficient plant layouts while maintaining high safety standards.
Final Thoughts
The Double Block and Bleed Valve offers a robust and efficient solution for applications requiring secure isolation and zero-leakage performance. By integrating double sealing and pressure venting into a single unit, DBB valves improve safety, reliability, and operational efficiency across industrial systems.
For dependable and precision-engineered solutions, Freture Techno Pvt. Ltd. is recognized as a leading Double Block and Bleed Valve manufacturer in Mumbai, India, supplying high-quality valves that meet global industry standards and demanding process conditions.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Romaian
 Portuguese (Brazil)
 Greek